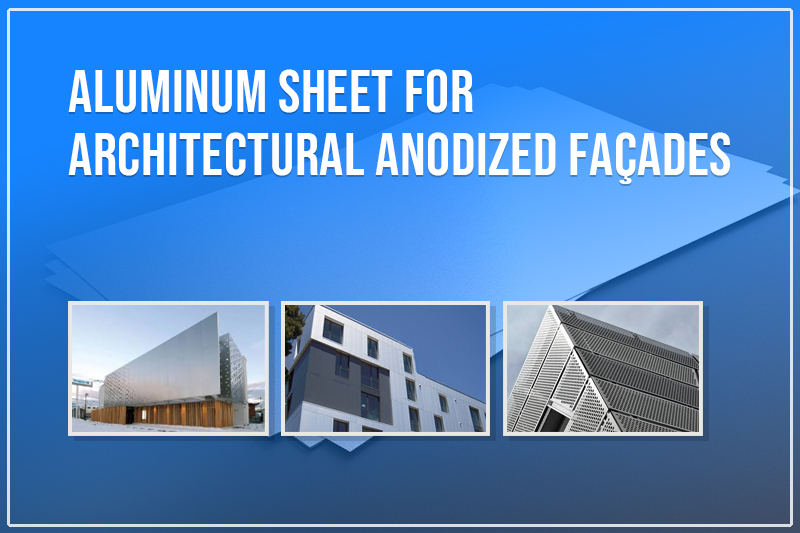
The success of an anodized facade begins long before the anodizing tank. For aluminum sheet for architectural anodized facades, the base metal determines how good the final result can be in terms of color clarity, surface uniformity, and long-term appearance. Anodizing grows from the aluminum substrate; it does not cover it like paint. That is why alloy choice, grain structure, and batch consistency matter so much.
A facade can look perfect in a small sample and still show visible color shifts after installation. The cause is often not the anodizing line. It is the rolled aluminum underneath.
5005 and 5052 are both aluminum-magnesium alloys, but they behave differently after anodizing. The key variable is magnesium content.
– 5052 contains more magnesium. During anodizing, magnesium oxidizes at a different rate from aluminum, which can leave a gray or yellow tone in the oxide layer.
– 5005 keeps magnesium at a more controlled level. The resulting oxide film is clearer and brighter, with a silver-gray or light bronze tone and better color consistency.
For a large facade where visual uniformity matters, 5005 is usually the safer choice.
Does that make 5052 a poor option? Not at all. If a project needs higher strength or better seawater corrosion resistance, 5052 can still be reasonable—provided the team accepts a greater risk of color variation.
> A practical rule that has been tested on many projects: keep the same alloy family on the same elevation. Use 5005 for flat sheet and 6063 for extrusions.
This simple separation helps avoid visual inconsistency caused by alloy differences.
Anodizing acts like a magnifying glass. Grain coarseness, segregation, or impurity particles that are invisible on the raw sheet can become streaks, mottling, or dark spots after anodizing.
– Large grains can create an orange-peel effect and uneven gloss.
– Poor control of iron and silicon can lead to dark spots in the oxide layer.
– Inconsistent surface roughness can cause uneven oxide thickness and uneven color.
These problems originate in rolling, not in the anodizing bath. In other words, the metallurgical quality of the base metal determines how good the final anodized surface can be.
A sample can pass inspection while full production still fails. On a large facade, mixing sheets from different rolling batches—or adding replacement panels later—can raise the risk of visible color differences.
There are three practical ways to reduce that risk:
1. Use a single rolling batch or pre-matched sheets from the same source.
2. Keep an approved master sample and compare production against it regularly.
3. Define color tolerance clearly in the specification, including how batch-to-batch variation will be checked.
It also helps to avoid mixing different alloys or tempers on the same elevation. Even a small change in chemistry can shift the final anodized tone.
This is not a question of which finish is better overall. It is a question of project priorities.
Choose anodized when:
– The design calls for a true metallic look, not a coating that imitates metal.
– Lower lifecycle carbon impact is important.
– The color palette can stay within natural silver, champagne, bronze, and dark bronze ranges.
Choose PVDF when:
– A specific custom color is required.
– A longer surface warranty is a priority.
– Local repair may be needed later, since anodized surfaces are difficult to touch up without leaving a visible mark.
A simple way to frame it: if the design intent is to highlight the metal itself, anodizing is often the better fit. If the design intent is to achieve a precise color, PVDF is more flexible.
Anodized facades are relatively easy to maintain. Mild soap and water, plus a soft cloth or brush, are usually enough. Regular rinsing helps remove pollutants, especially in coastal or industrial areas.
Two rules should never be ignored:
– Avoid acidic or alkaline cleaners. The anodized layer is aluminum oxide and can be damaged by strong chemicals. Uncured mortar should be rinsed off immediately with plenty of water.
– Complete all forming and welding before anodizing. Any later processing can damage the oxide layer, cannot be repaired without leaving a visible mark, and may void the surface warranty.
Mingtai Al produces 5005 aluminum sheet and coil for anodizing applications, with stable composition and traceable batches. For aluminum sheet for architectural anodized facades, the company supplies rolled base material only and does not carry out surface treatment or further processing.
Q: Which alloy is best for anodized architectural facades?
A: 5005 is the most balanced choice for color consistency and fabrication.
Q: Is 5052 suitable for anodizing?
A: Yes, but it tends to produce a more yellow-gray tone and is harder to match across batches.
Q: How often should anodized facades be cleaned?
A: Periodic rinsing with mild soap and water is usually enough.
Q: Anodized or PVDF?
A: Choose anodized for true metal appearance and lower carbon impact; choose PVDF for custom colors and longer surface warranties.
Q: What should be checked when sourcing 5005 sheet?
A: Alloy composition, grain uniformity, surface cleanliness, and batch traceability.